
Call Us
+86 136 6007 9809
Call Us
+86 136 6007 9809

Oct. 22, 2023
Insulation weld pins are welded fastening components used to mechanically retain thermal or acoustic insulation on compatible metal substrates.
A typical insulation fastening system consists of:
metal substrate → welded insulation pin → insulation layer → retaining washer or speed clip
Instead of treating the pin as a conventional screw, engineers should evaluate the complete fastening system: the welding method, base-metal compatibility,
insulation thickness, pin length, retaining washer, installation process and required holding performance.
JUXIN FASTENERS supplies insulation weld pins, weld studs, insulation retaining washers,
self-locking washers and drawing-based fastening components for HVAC equipment, industrial machinery, food-service equipment, thermal management systems and other OEM assemblies.
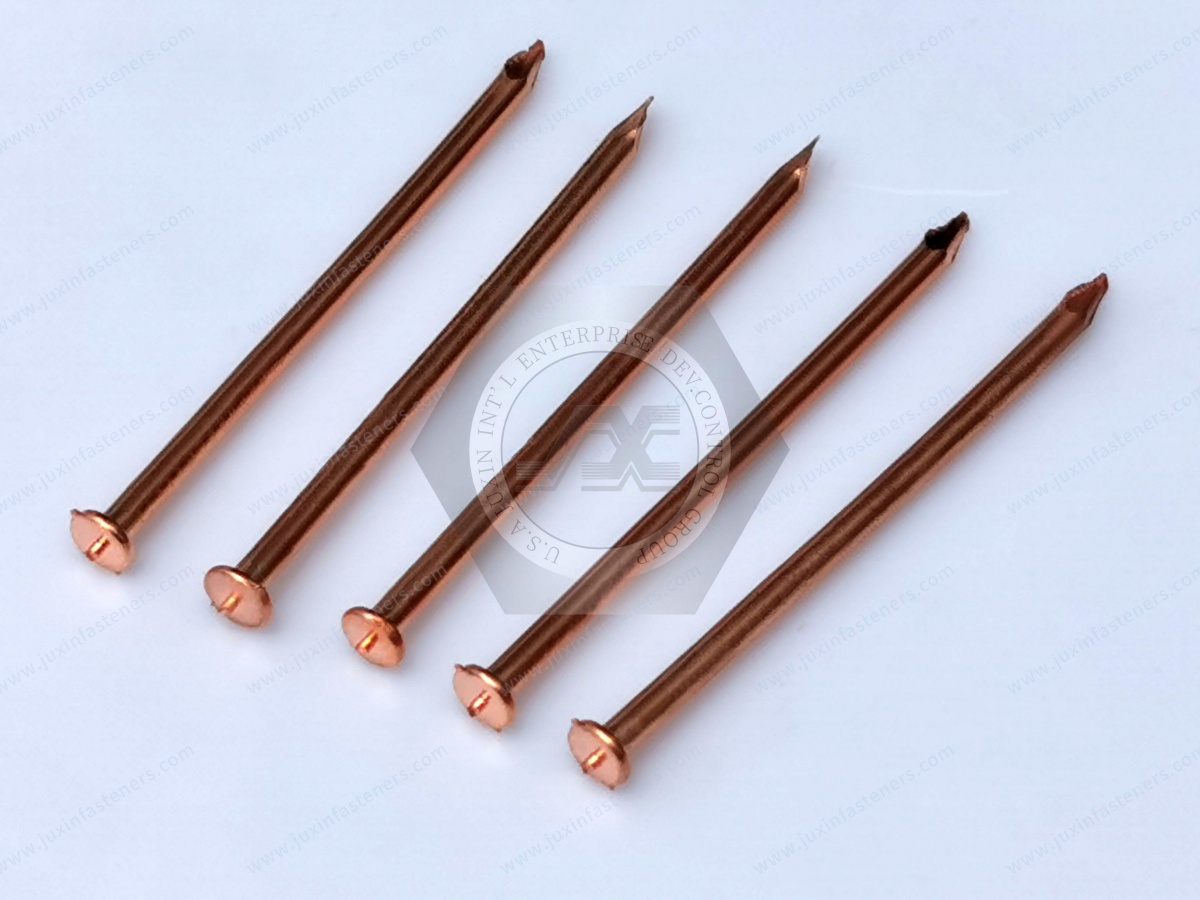
An insulation weld pin is a metal pin designed to be welded directly to a compatible metallic surface so that insulation can be positioned over the pin and mechanically retained.
Depending on the product design and installation process, weld pins may be associated with capacitor discharge welding or another specified stud-welding process.
After the pin has been welded to the substrate:
the insulation is positioned over the pin;
the pin passes through the insulation;
a compatible retaining washer or speed clip is pressed onto the pin;
the insulation is mechanically held against the substrate.
The pin itself does not need to "melt through" the insulation.
Its function is to create a welded anchoring point on the metal substrate.
These terms describe two different things.
The fastener that remains in the final assembly.
The installation equipment used to create the welded connection between the pin and the compatible metal substrate.
For procurement purposes, this distinction is important.
A company sourcing insulation fasteners may need:
weld pins;
insulation retaining washers;
speed clips;
application-specific pin dimensions;
material and finish requirements;
without purchasing the welding equipment itself.
The mechanical fastening path is straightforward:
substrate → weld joint → pin → retaining washer → insulation
Each interface has a different function.
Provides the base surface to which the pin is welded.
Creates the permanent connection between the pin and compatible base material.
Provides the mechanical stem through the insulation layer.
Can include suitable thermal or acoustic insulation specified by the equipment designer.
Engages the pin and distributes retaining force over an area of the insulation.
Understanding this complete system is more useful than specifying the weld pin independently.
Capacitor discharge, commonly abbreviated CD, is one stud-welding process used for suitable small-diameter studs and pins.
In a CD welding system, stored electrical energy is discharged over a very short welding cycle to create the weld at the interface between the fastener and compatible metal substrate.
The exact:
equipment setting;
electrical energy;
pin geometry;
substrate thickness;
material combination;
surface condition;
must be matched to the welding system and validated for the application.
There is no universal welding setting that should be applied to every insulation pin.
A common misunderstanding is that insulation welding works by heating an entire pin until it melts.
That is not an accurate description of stud welding.
The process is intended to create a controlled metallurgical connection at the interface between the weld fastener and the base metal.
The fastening result therefore depends on the complete combination of:
fastener + welding process + substrate + surface condition + equipment settings
This distinction is important for engineering qualification.
Not all insulation pins use the same attachment method.
The pin is metallurgically joined to a compatible metal substrate.
Potential advantages for appropriate applications include:
mechanical attachment directly to the substrate;
no adhesive curing stage;
suitability for production-oriented metal assemblies;
compatibility with retaining washers.
The pin is attached using an adhesive-backed or bonded base.
These may be useful where welding is unavailable or inappropriate.
However, their performance depends on additional factors such as:
adhesive system;
surface preparation;
temperature;
substrate condition;
environmental exposure.
Neither system should automatically be described as universally better.
The attachment method should match the substrate, production process and service environment.
Self-sticking insulation hangers use an adhesive attachment rather than a welded joint.
They can simplify installation in some field applications but should not automatically be substituted for weld pins.
For OEM equipment manufacturing, engineers should consider:
substrate material;
manufacturing sequence;
expected temperature;
service environment;
required retention;
installation volume;
production automation.
An insulation weld pin generally provides a smooth or application-specific stem for retaining insulation with a compatible washer or clip.
A threaded weld stud provides a threaded attachment point for a nut or another threaded component.
Both may use welding technology, but their downstream fastening functions are different.
The insulation retaining washer is not simply an accessory.
It is the component that transfers retaining force from the pin into the insulation material.
Its geometry can influence:
contact area;
resistance to pull-through;
interaction with soft insulation;
installation force;
final retention.
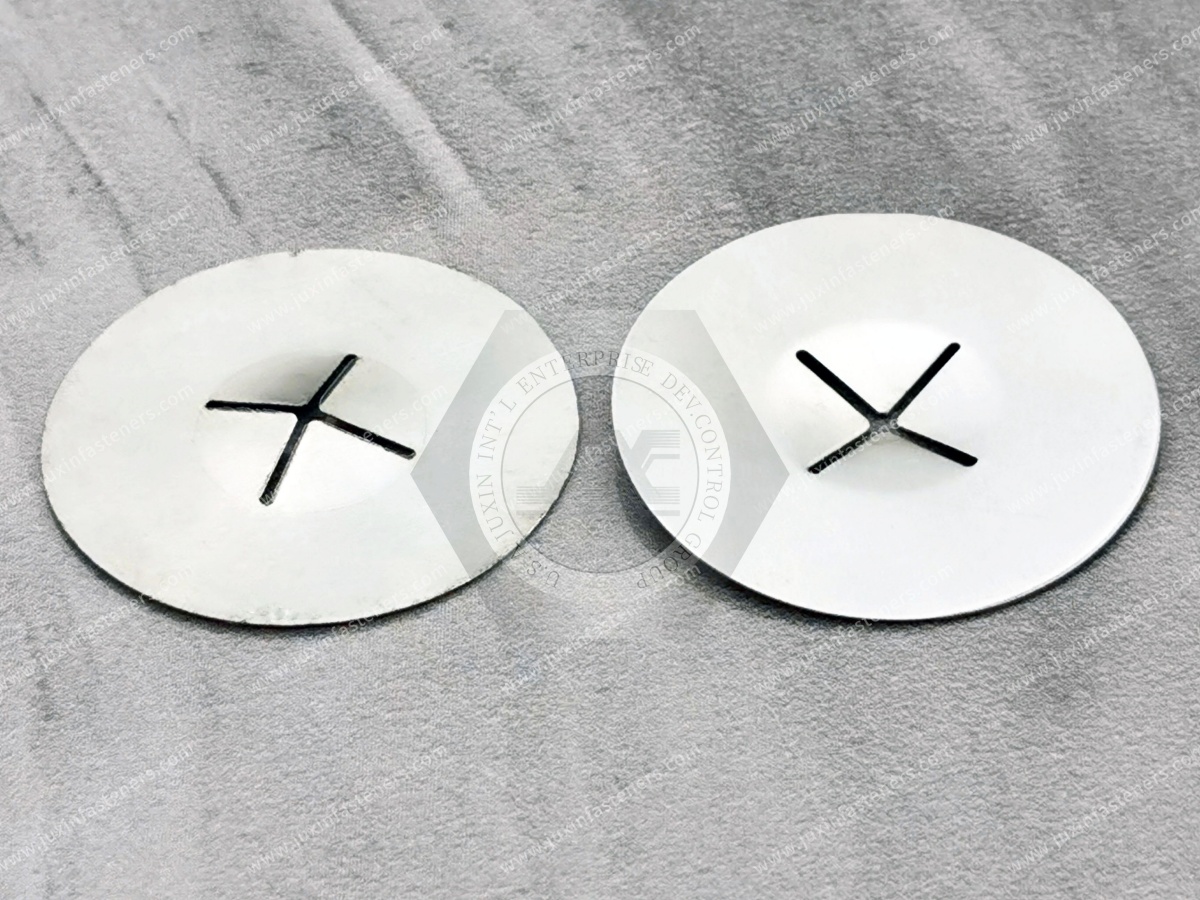
JUXIN FASTENERS also supplies stainless steel insulation retaining washers for suitable OEM applications.
Available designs can be developed according to pin diameter, washer outside diameter, thickness and customer drawing requirements.
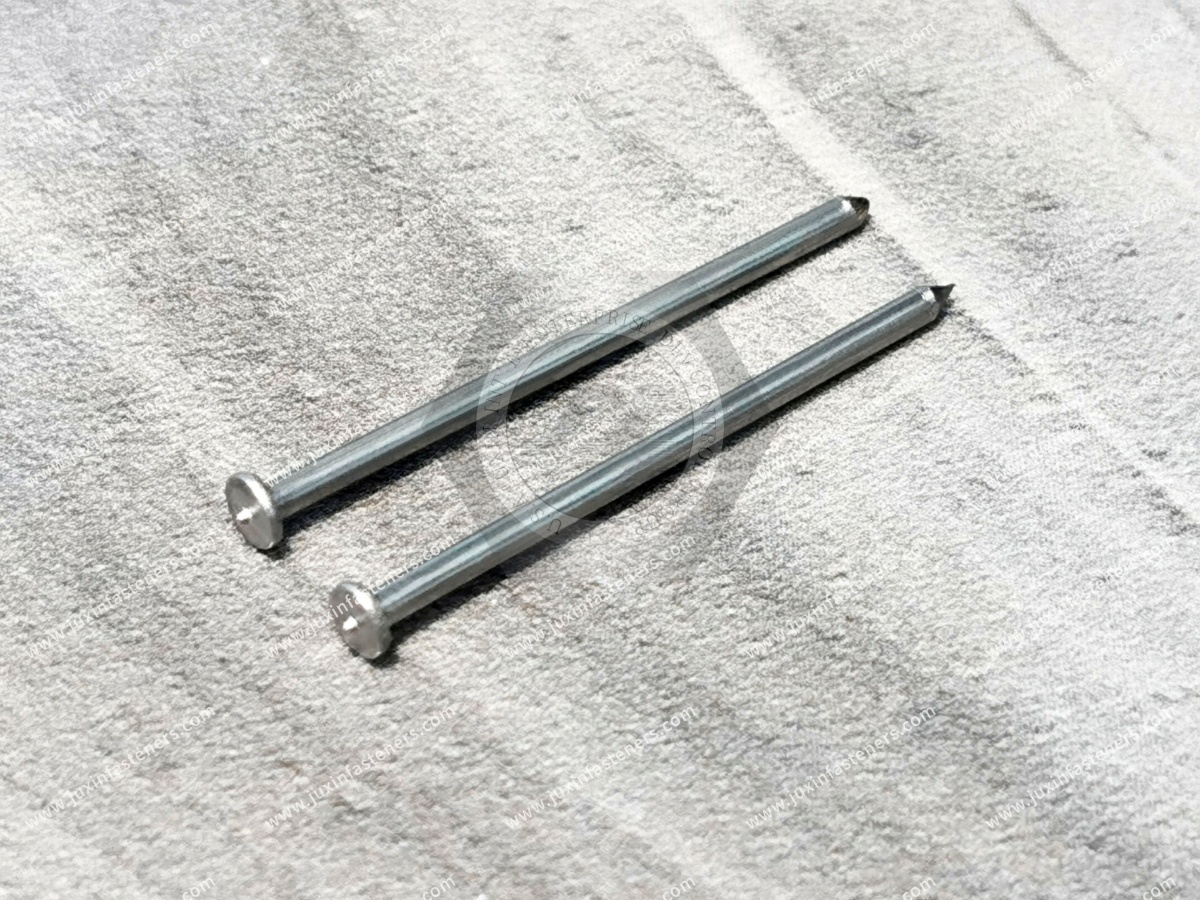
A self-locking retaining washer typically contains an internal gripping feature that allows it to be pushed onto the insulation pin.
Once installed, the internal geometry resists movement in the reverse direction.
This creates a simple assembly sequence:
weld pin → install insulation → push washer onto pin
The exact retention performance depends on:
pin diameter;
washer geometry;
washer material;
material thickness;
manufacturing tolerances;
installation condition.
These variables should be evaluated together.
The correct pin should not be selected by length alone.
Engineers should evaluate several variables.
First determine the material to which the pin will be welded.
Weldability and process compatibility depend on the actual material combination.
Do not assume every pin material can be welded successfully to every sheet-metal substrate.
Thin sheet creates different welding constraints from thicker structural material.
The selected weld process, pin geometry and equipment settings must be compatible with the substrate.
For thin-wall HVAC housings, cabinets and equipment panels, this can be particularly important.
The pin must provide sufficient usable length for:
insulation thickness + retaining washer engagement + required installation allowance
The correct allowance depends on the actual washer and assembly design.
Avoid applying a universal extra-length rule to every insulation system.
Soft fibrous insulation behaves differently from dense insulation material.
The designer should consider whether the retaining washer:
compresses the insulation excessively;
provides adequate contact area;
risks pulling through the insulation;
maintains the intended insulation thickness.
Pin diameter affects compatibility with the retaining washer.
The washer gripping geometry must match the specified pin diameter.
A washer that is too loose may not retain correctly.
A washer that is too tight may require excessive installation force or damage the pin/washer interface.
Material selection should consider:
weld-process compatibility;
substrate compatibility;
corrosion environment;
temperature;
OEM specification.
Oil, coatings, oxidation and contamination can influence welding consistency.
The manufacturing process should define appropriate surface preparation and welding qualification.
For an insulation retaining washer, evaluate:
pin diameter;
washer outside diameter;
washer thickness;
internal gripping geometry;
material;
corrosion requirements;
insulation type;
required contact area.
Large-diameter retaining washers can distribute force across a broader insulation area, which may be useful for softer insulation systems.
However, washer diameter should be selected according to the actual insulation and equipment geometry.
Stainless steel retaining washers can be useful in equipment exposed to:
moisture;
cleaning;
humidity;
elevated corrosion requirements.
Examples can include certain:
food-service equipment;
commercial kitchen equipment;
HVAC systems;
thermal insulation assemblies;
industrial enclosures.
Material selection should still be based on the actual environmental and customer specification.
"Stainless steel" alone does not define the complete performance requirement.
HVAC equipment frequently contains insulated sheet-metal structures where thermal and acoustic control are important.
Potential applications include:
air-handling equipment;
duct sections;
ventilation equipment;
fan housings;
equipment cabinets;
insulated sheet-metal panels.
Weld pins can provide a production-oriented method for attaching insulation where the substrate and manufacturing process are compatible with welding.
Commercial food-service equipment can require insulation around heated or temperature-controlled assemblies.
Fastening systems may need to consider:
stainless steel construction;
cleaning environment;
thermal cycling;
corrosion resistance;
equipment serviceability.
JUXIN FASTENERS supplies insulation retaining washers and other fastening components for suitable industrial equipment applications.
Machine housings and equipment enclosures can use insulation for:
thermal control;
acoustic attenuation;
personnel protection;
process-temperature management.
Where sheet-metal construction permits welding, insulation pins and retaining washers can provide a mechanically retained insulation architecture.
Equipment involving controlled heat flow may require insulation around:
housings;
ducts;
enclosures;
thermal barriers;
process assemblies.
Fastener material and geometry should be selected as part of the complete thermal design rather than independently.
Insulation fasteners can also be used with suitable acoustic materials.
For acoustic applications, the engineer should consider whether the fastener and retaining washer:
compress the material;
create local hard points;
interfere with acoustic performance;
remain compatible with vibration.
The fastening solution should support—not compromise—the intended insulation system.
A typical weld-pin insulation assembly can follow this sequence.
Confirm:
pin location;
pin spacing;
pin length;
pin diameter;
material;
retaining washer;
substrate specification.
The welding surface should meet the requirements of the selected welding process.
Surface contamination that affects welding should be controlled.
Use qualified settings for the actual:
pin;
substrate;
equipment;
material combination.
Position the pin according to the drawing and create the weld using the specified process.
Inspection requirements should follow the applicable manufacturing or customer specification.
Place the insulation over the installed pins.
Push the compatible retaining washer or clip onto each pin until the insulation is retained at the intended position.
Check:
insulation position;
washer engagement;
damaged insulation;
loose pins;
incomplete retention;
other customer-defined acceptance criteria.
There is no universal pin-spacing rule suitable for every insulation application.
Required pin quantity and spacing can depend on:
insulation weight;
insulation stiffness;
orientation;
vibration;
equipment geometry;
service environment;
retaining washer size;
customer specification.
For this reason, JUXIN FASTENERS should not prescribe a universal spacing without reviewing the application.
The equipment designer or approved installation specification should define the fastening pattern.
Weld performance is not determined by the pin alone.
Important variables include:
pin design;
pin material;
substrate material;
substrate thickness;
surface condition;
welding equipment;
welding parameters;
operator/process control.
For critical OEM programs, the welding process should be qualified using the actual production material combination.
The retaining washer may not achieve the intended engagement after passing through the insulation.
Excess projection can interfere with packaging, covers, service access or downstream assembly.
Incorrect internal gripping geometry can cause poor retention or excessive installation force.
Excessive compression can alter insulation thickness and potentially affect thermal or acoustic performance.
Inconsistent substrate condition or welding parameters can produce variable attachment quality.
The selected fastener and substrate may not be suitable for the intended welding process.
The washer contact area may be insufficient for the insulation characteristics or loading condition.
For a new insulation fastening application, use the following sequence:
1. What is the substrate material and thickness?
↓
2. Is welding an appropriate attachment method?
↓
3. Which welding process is specified?
↓
4. What insulation material and thickness must be retained?
↓
5. What pin diameter and length are required?
↓
6. What retaining washer geometry matches the pin and insulation?
↓
7. What corrosion and temperature conditions apply?
↓
8. What pin spacing does the equipment design require?
↓
9. How will the weld and final insulation assembly be inspected?
This system-level approach is more reliable than selecting a weld pin from diameter and length alone.
Standard insulation pins can be suitable where common dimensions meet the assembly requirement.
Custom components may be appropriate when an OEM requires:
non-standard length;
specific pin diameter;
special head or weld geometry;
specific material;
particular surface finish;
unique retaining washer interface;
drawing-controlled dimensions;
dedicated packaging.
For high-volume equipment manufacturing, the pin and retaining washer can be evaluated as a matched fastening system.
Procurement teams evaluating an insulation fastener supplier should look beyond unit price.
Important considerations can include:
drawing control;
dimensional consistency;
material specification;
washer-to-pin compatibility;
sample approval;
production repeatability;
lot identification;
packaging;
supply continuity.
A low-cost pin that does not match the retaining washer or production welding process can create much larger assembly costs downstream.
Different decision-makers search for insulation fasteners differently.
Engineers may search:
how do insulation weld pins work;
CD weld pins for insulation;
weld pin length for insulation;
insulation pin and speed clip selection;
HVAC insulation fastening method;
weld pins vs adhesive pins;
retaining washer for insulation pin.
Their primary question is:
Will this fastening system work with my substrate, insulation and manufacturing process?
Procurement teams may search:
insulation weld pin supplier;
HVAC insulation fastener manufacturer;
CD weld pin manufacturer;
insulation retaining washer supplier;
custom insulation pin manufacturer;
stainless steel insulation washer supplier.
Their primary question is:
Can the supplier manufacture the correct pin-and-washer system consistently and at production volume?
A successful OEM supply program must satisfy both.
For faster engineering review and quotation, provide:
weld pin drawing or reference;
pin diameter;
pin length;
pin material;
surface finish if applicable;
welding process;
substrate material;
substrate thickness;
insulation type;
insulation thickness;
retaining washer dimensions;
retaining washer material;
application;
operating environment;
quantity per order;
estimated annual volume;
inspection requirements;
packaging requirements.
If the current product is being replaced, provide the original sample and mating retaining washer where possible.
It is a metal fastening pin welded to a compatible substrate and used with a retaining washer or clip to mechanically hold insulation.
Not necessarily. Many insulation weld pins are non-threaded pins designed specifically for welded insulation-retention systems.
No. A controlled welding process creates the connection at the fastener-to-substrate interface.
It is a pin designed for a compatible capacitor-discharge stud-welding process.
A compatible insulation retaining washer or speed clip is typically installed over the pin.
Pin length should be determined from the insulation thickness, retaining-washer engagement and the actual assembly requirements. There is no universal allowance for every application.
No. Washer gripping geometry must be compatible with the pin diameter and design.
Neither method is universally better. Selection depends on substrate, production method, service environment, installation volume and engineering requirements.
No. Welding-process compatibility must be evaluated for the actual pin, substrate material, thickness and surface condition.
Yes. JUXIN FASTENERS supplies insulation retaining washers and can support drawing-based insulation fastening components for suitable OEM applications.
For engineers, insulation fastening should be evaluated as a complete system:
metal substrate + welding process + weld pin + insulation + retaining washer
For procurement teams, pin dimensions alone are not enough. The supplier should understand the relationship between the weld pin, substrate, insulation thickness and retaining washer.
JUXIN FASTENERS supplies insulation weld pins, weld studs, insulation retaining washers, self-locking washers and custom fastening components for HVAC,
food-service equipment, thermal management, industrial machinery and other OEM applications.
For standard products, send the required size, material, quantity and application.
For custom components, send the 2D drawing or 3D model together with substrate and insulation information.
For replacement projects, send an unused sample where possible together with the mating retaining washer.
We can support technical review, sample evaluation, manufacturing feasibility, custom development, quotation, sample qualification and volume production.
Email: info@juxinfasteners.com
Website: www.juxinfasteners.com
Previous: Insulation Welding Pins Guide
 MORE NEWS

Sep. 27, 2026

Sep. 27, 2026

Sep. 27, 2026
Contact Us
Tel.:
+86 020 8621 0320
+86 020 3121 6067
E-mail:
Technical Support:
Navigation
SEND INQUIREY